
General Overhaul of a Low-Pressure Casting Furnace
Not a melting furnace with a lid, but a pressure vessel
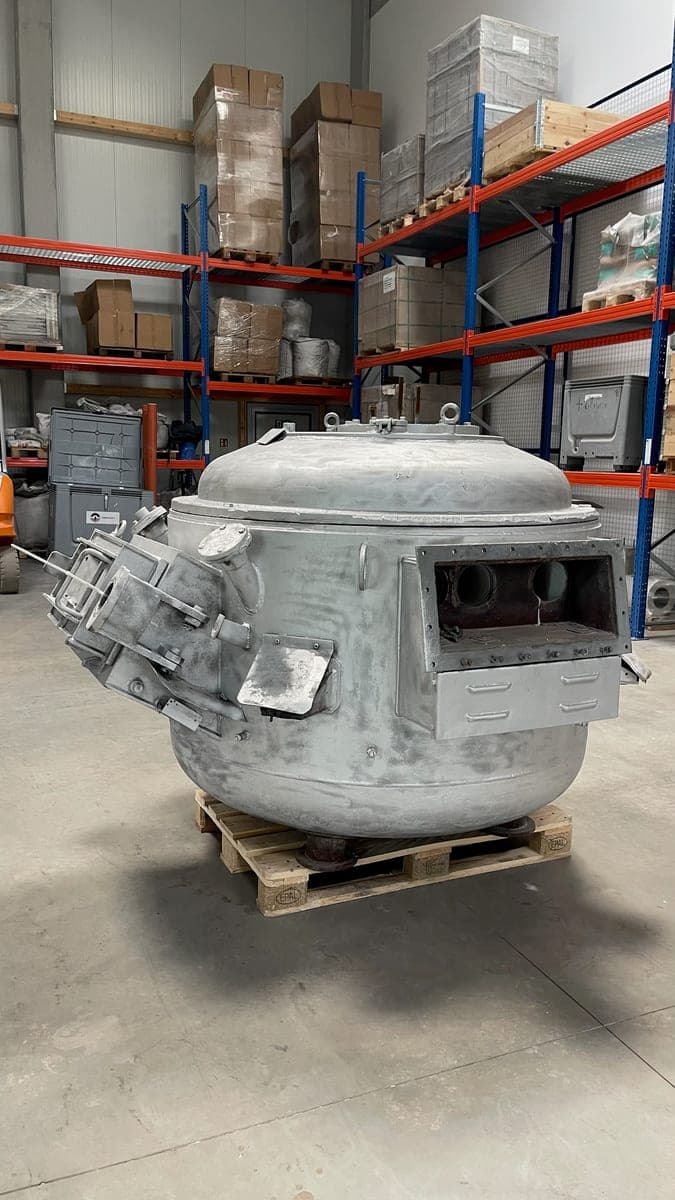
Initial situation
A low-pressure casting furnace is a closed pressure vessel: above the aluminium bath there is a gas overpressure of around 0.2 to 0.7 bar, which pushes the melt through the riser tube into the die. The lining therefore not only has to withstand the melt, but must be part of a tight system. The furnace was collected from the customer and completely refurbished in the workshop.
Scope of services
- General overhaul
- Pressure tightness
- Riser tube seat
- Bath lining
- Workshop repair
Project data
The task
Lid, penetrations and sealing faces must remain gas-tight — every leak costs dosing accuracy
The seat of the riser tube, the most heavily loaded component, must be dimensionally accurate and tight
Aluminium must not infiltrate the bath lining, and corundum must not clog the cross-section
The SBS approach
After delivery, the furnace was cleared out, measured and inspected; the casing was blasted.
Lid, penetrations and sealing faces were renewed, and the riser tube seat was made dimensionally accurate and tight.
Non-wetting materials were used in the bath, and the new lining was cast monolithically in dimensionally precise formwork. The initial heat-up follows a defined heat-up curve with holding stages.
General Overhaul of a Low-Pressure Casting Furnace in pictures
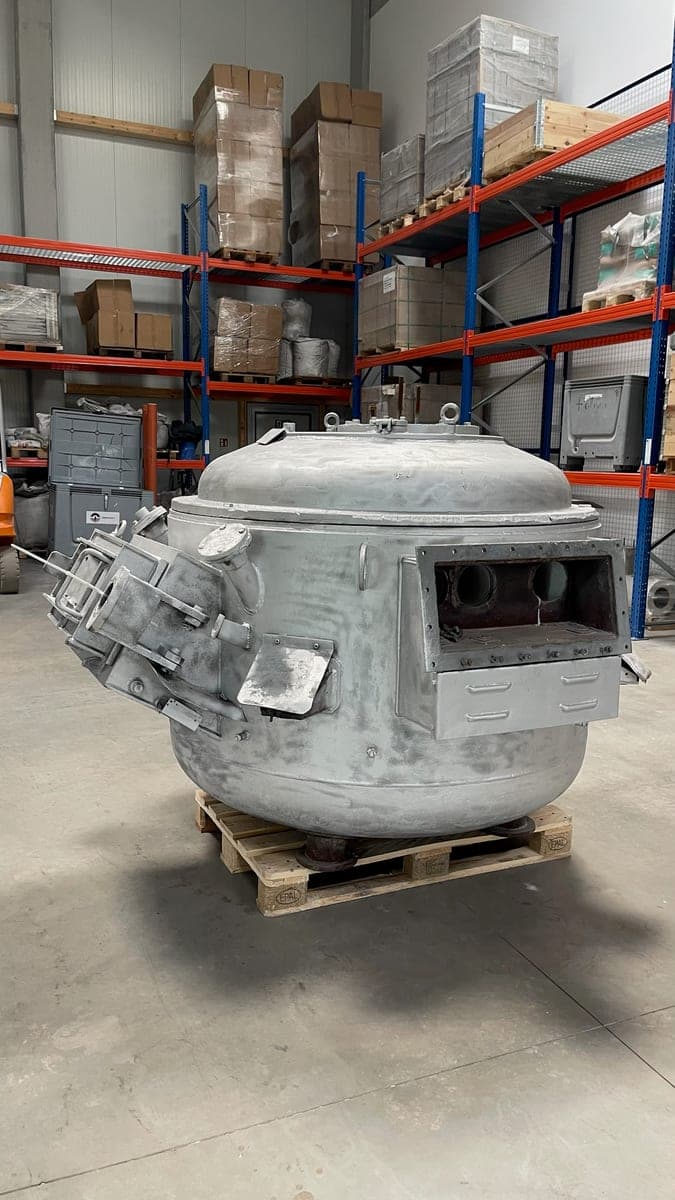
Fully overhauled, ready for delivery
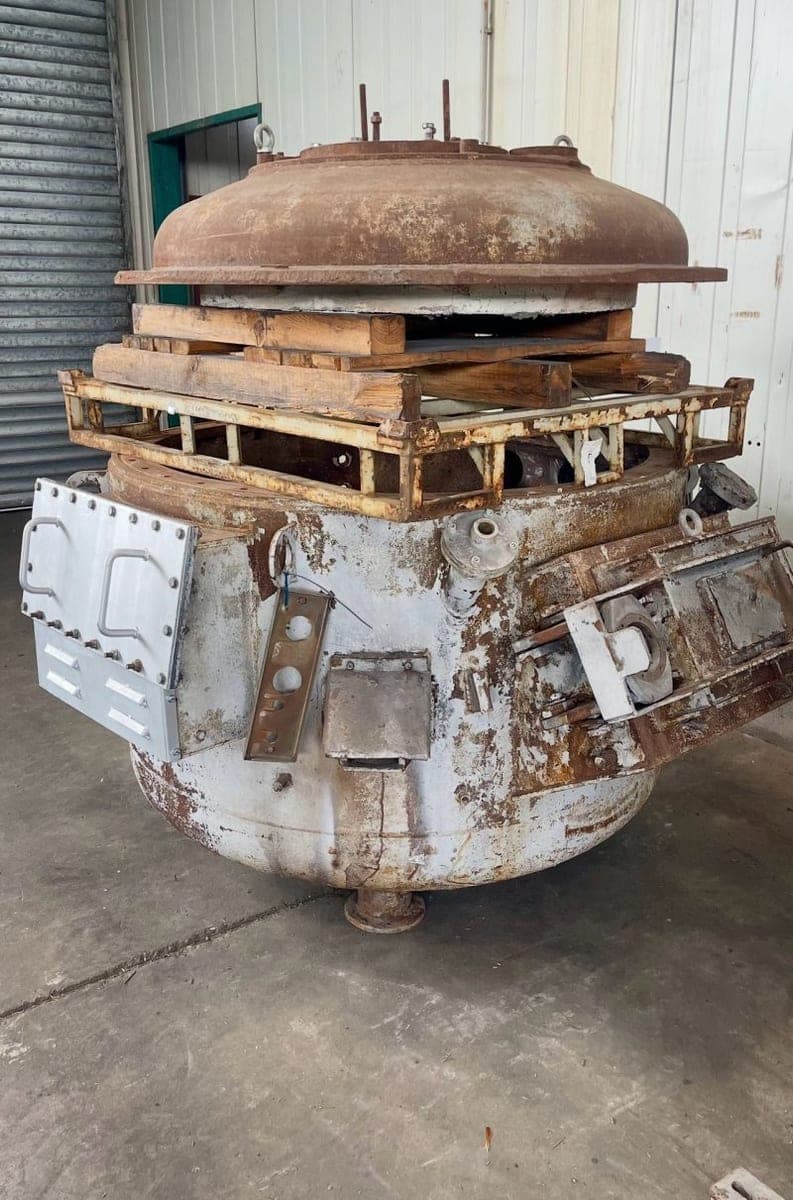
Condition on delivery
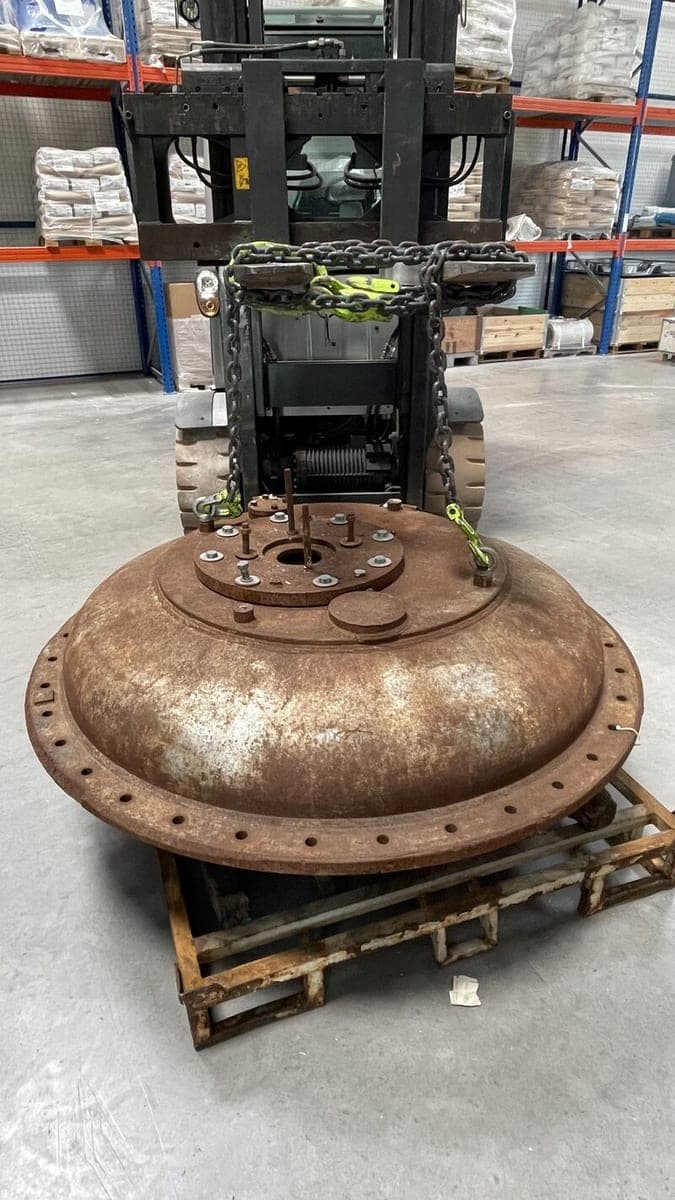
The lid — sealing faces and penetrations are being renewed
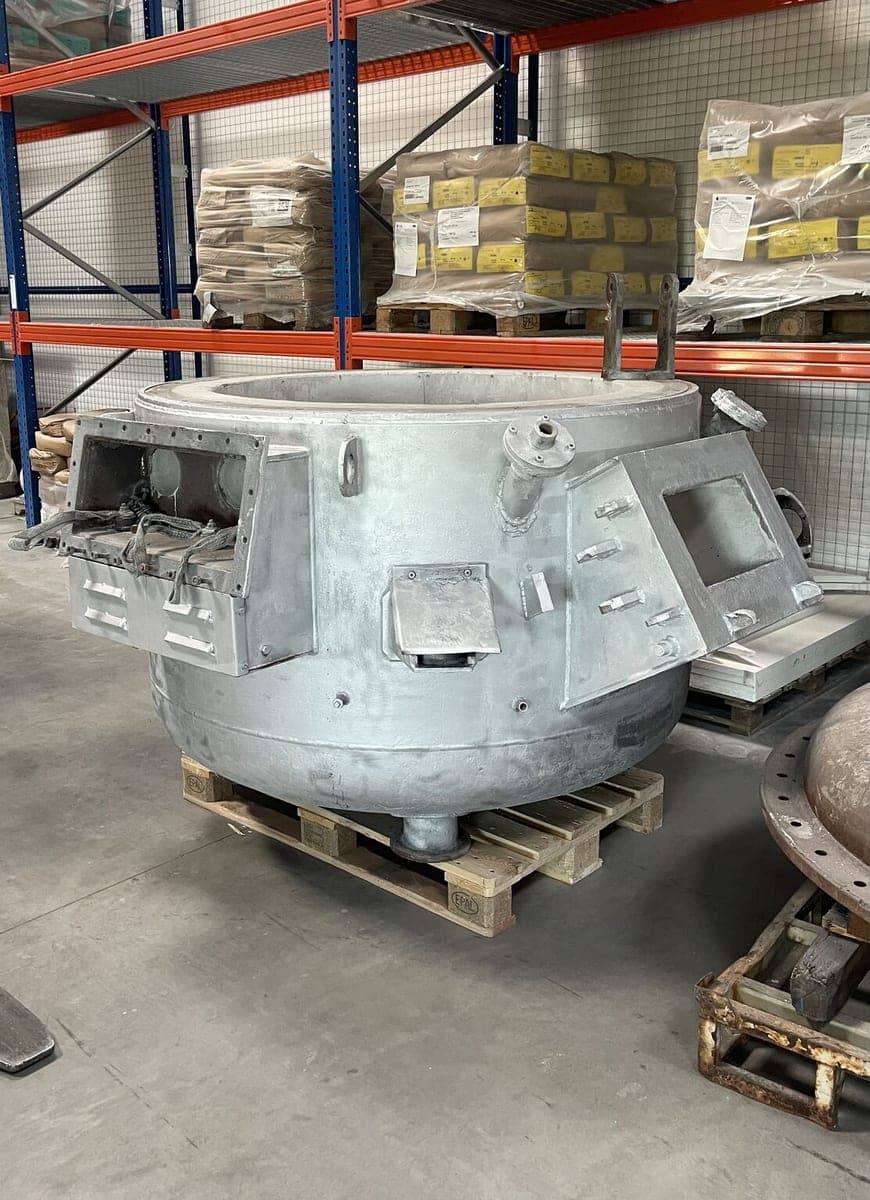
Casing blasted
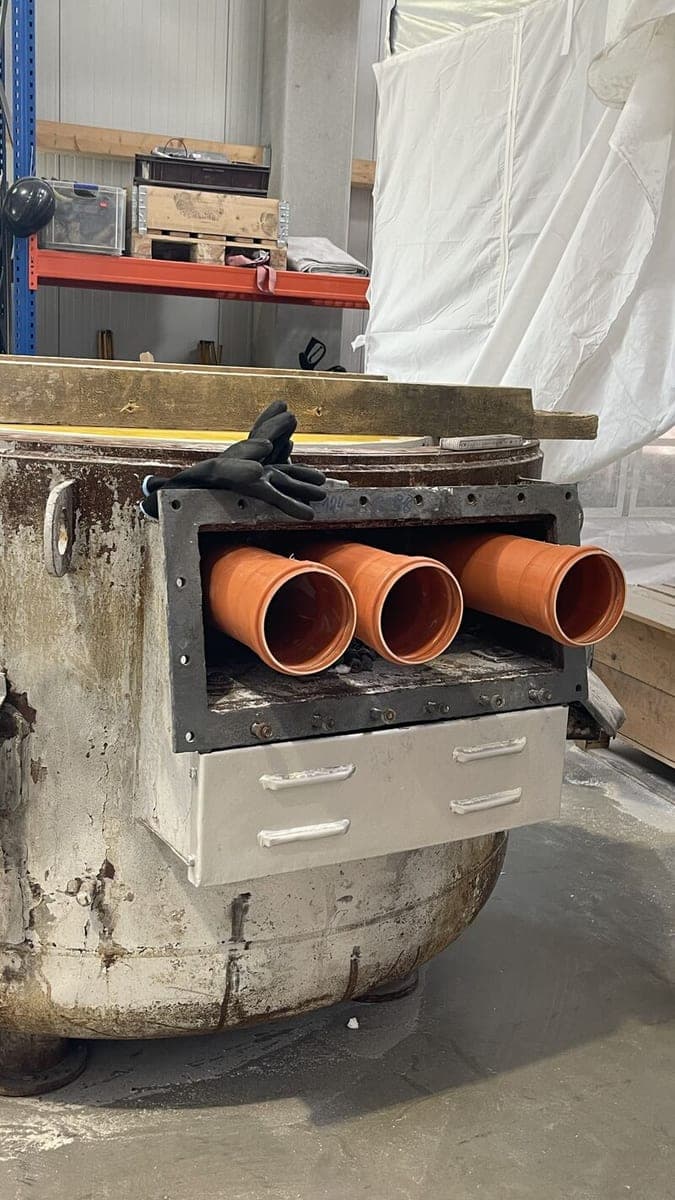
Detail at the furnace opening during repair
Measurable results
The key figures of the “General Overhaul of a Low-Pressure Casting Furnace” project
Similar references
Planning a project?
Whether complete relining, repair or emergency — free initial consultation and a fast response.